Facilitator guide
Case objectives, demonstration plans, debriefs, common mistakes and application checks across all 81 workplace cases and method lessons.
Download Facilitator guide PDF · 166 pages · 65.1 MB OPEXSTUDIO
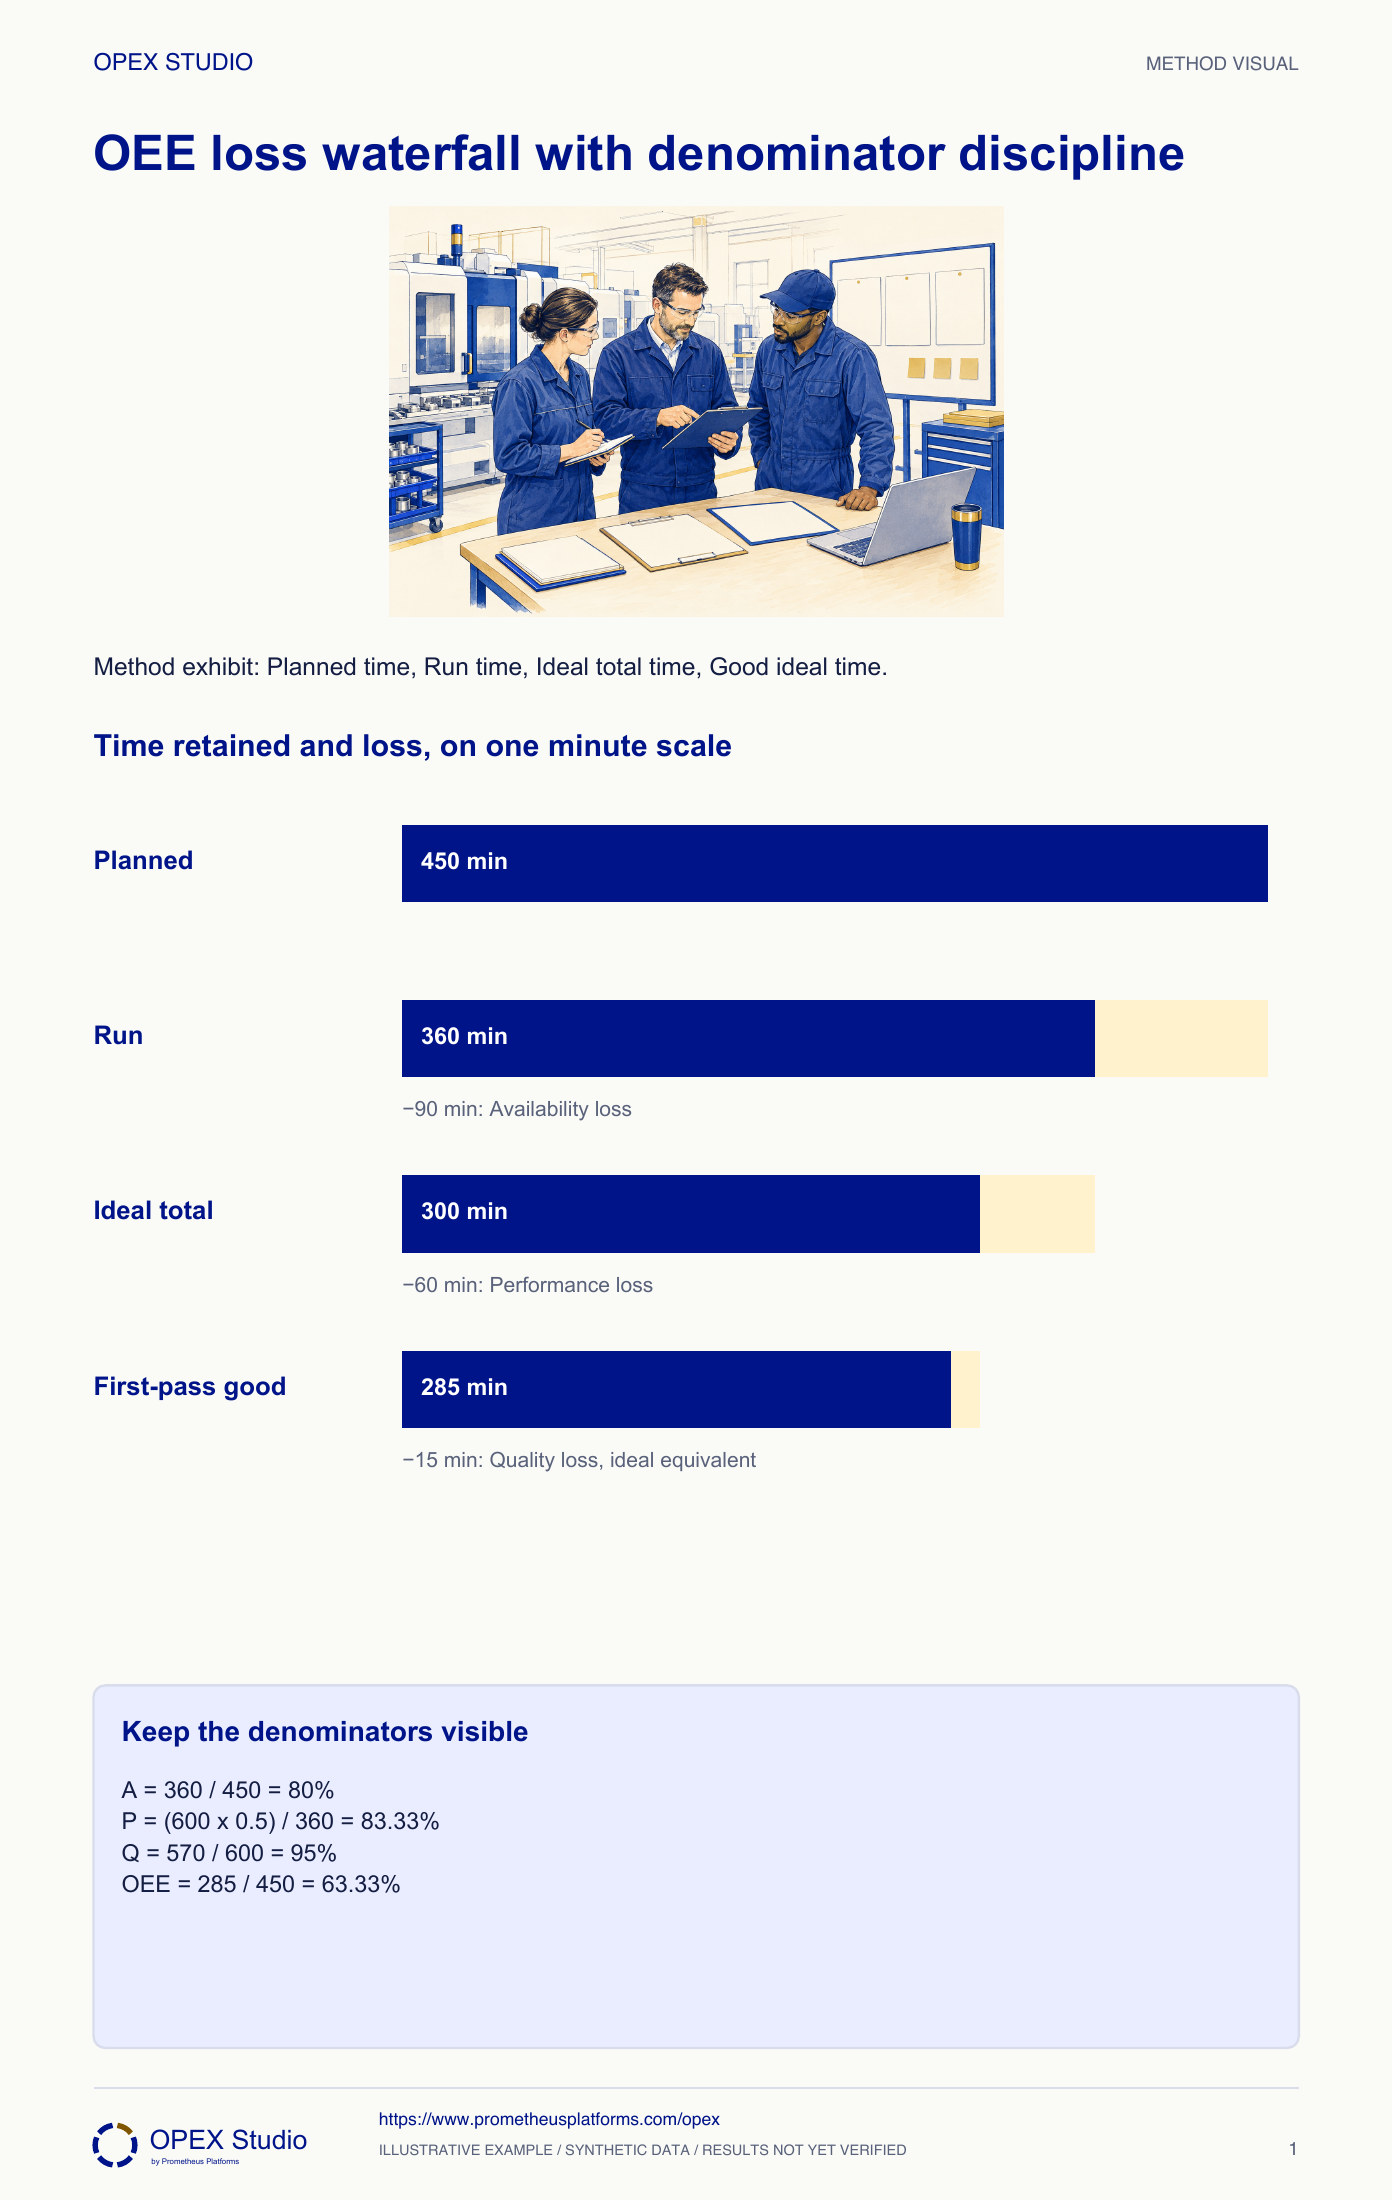
Overall equipment effectiveness (OEE) combines availability, performance and quality within a defined production-time boundary. Use this lesson to understand the losses behind the percentage. Work through the calculation, check the denominators and connect the largest relevant loss to an investigation rather than chasing a score alone.
Fictional teaching examples and AI-generated illustrations. Proposed changes and goals are not achieved results. Use the written instructions and check local conditions before applying a method.
Published by OPEX Studio, a Prometheus Platforms product. Read the method sources and their scope.
Declare the planned production time before calculating equipment effectiveness. In this exercise, 360 run minutes from 450 planned minutes gives 80% availability. Six hundred units at an ideal half-minute each represent 300 ideal minutes, giving 83.33% performance during run time. Of those units, 570 are good first time, giving 95% quality. Multiplying the three factors yields 63.33% OEE, equivalent to 285 good ideal minutes out of 450. Investigate the underlying loss rather than chasing the score. Reworked output is not first-pass good, and making unwanted inventory cannot establish better customer flow.
Availability 360/450 = 80%; performance (600 × 0.5)/360 = 83.33%; quality 570/600 = 95%.
OEE = 63.33%, equivalent to 285 first-pass-good ideal minutes / 450 planned minutes. Losses are 90 + 60 + 15 = 165 min.
Use first-pass good output; avoid double-counting losses or chasing local utilization when customer demand is absent.
Fictional machine-shift record: 450 minutes were planned for production, the machine ran 360 minutes and made 600 units, of which 570 were first-pass good. The approved ideal cycle for this exercise is 0.5 minute per unit. Analyst Tessa must explain the loss picture before recommending improvement work.
Keep first-pass quality at 570 / 600 = 95% for this defined original pass and record rework/recovery separately. Clarify how any rework resource/time enters the relevant reporting scope.
Recovery changes disposition, not first-pass history. Mixing scopes can count output or time twice.
Reconcile OEE factors and equivalent-time losses, retain first-pass quality accounting and choose a loss investigation without mistaking the percentage for a cause.
Fictional machine-shift record: 450 minutes were planned for production, the machine ran 360 minutes and made 600 units, of which 570 were first-pass good. The approved ideal cycle for this exercise is 0.5 minute per unit. Analyst Tessa must explain the loss picture before recommending improvement work.
Role: Production analyst with operator, quality and maintenance representatives.
Time scope, count definitions and ideal cycle are explicit and consistent; the factors reconcile to good ideal time divided by planned time.
The dashboard shows a low result but the team is treating all lost time as downtime and counting reworked units as first-pass good.
| Input | Supplied value |
|---|---|
| Planned production time | 450 min |
| Run time | 360 min |
| Total units | 600 |
| First-pass good units | 570 |
| Ideal cycle | 0.5 min/unit |
| Non-first-pass units | 30; disposition does not change first-pass history |
Divide 360 run minutes by 450 planned minutes to obtain 80%. The difference is 90 minutes of availability loss under the supplied time definition.
Why: The denominator must remain the agreed planned scope; removing a loss from the denominator would improve the number without improving the work.
Evidence: 450 = 360 + 90 minutes.
600 total units at 0.5 ideal minute require 300 ideal minutes. Divide 300 by 360 run minutes to obtain 83.33% performance.
Why: Performance compares ideal output time with run time; it is not another downtime subtraction.
Evidence: 360 minus 300 = 60 minutes performance loss equivalent.
Divide 570 first-pass good units by 600 total units to obtain 95% quality. Good ideal time is 570 × 0.5 = 285 minutes.
Why: Later rework may recover product but does not undo the original failure to be good first pass.
Evidence: 300 minus 285 = 15 minutes quality loss at ideal time.
Multiply 0.80 × 0.833333… × 0.95 = 0.633333…, or 63.33%. Check 285 / 450 gives the same result. Review loss events with the responsible teams before selecting an investigation.
Why: OEE locates loss categories but does not identify a failed component, prove a cause or justify maximizing every machine’s output.
Evidence: 90 + 60 + 15 + 285 = 450 minutes; actual causes require event evidence.
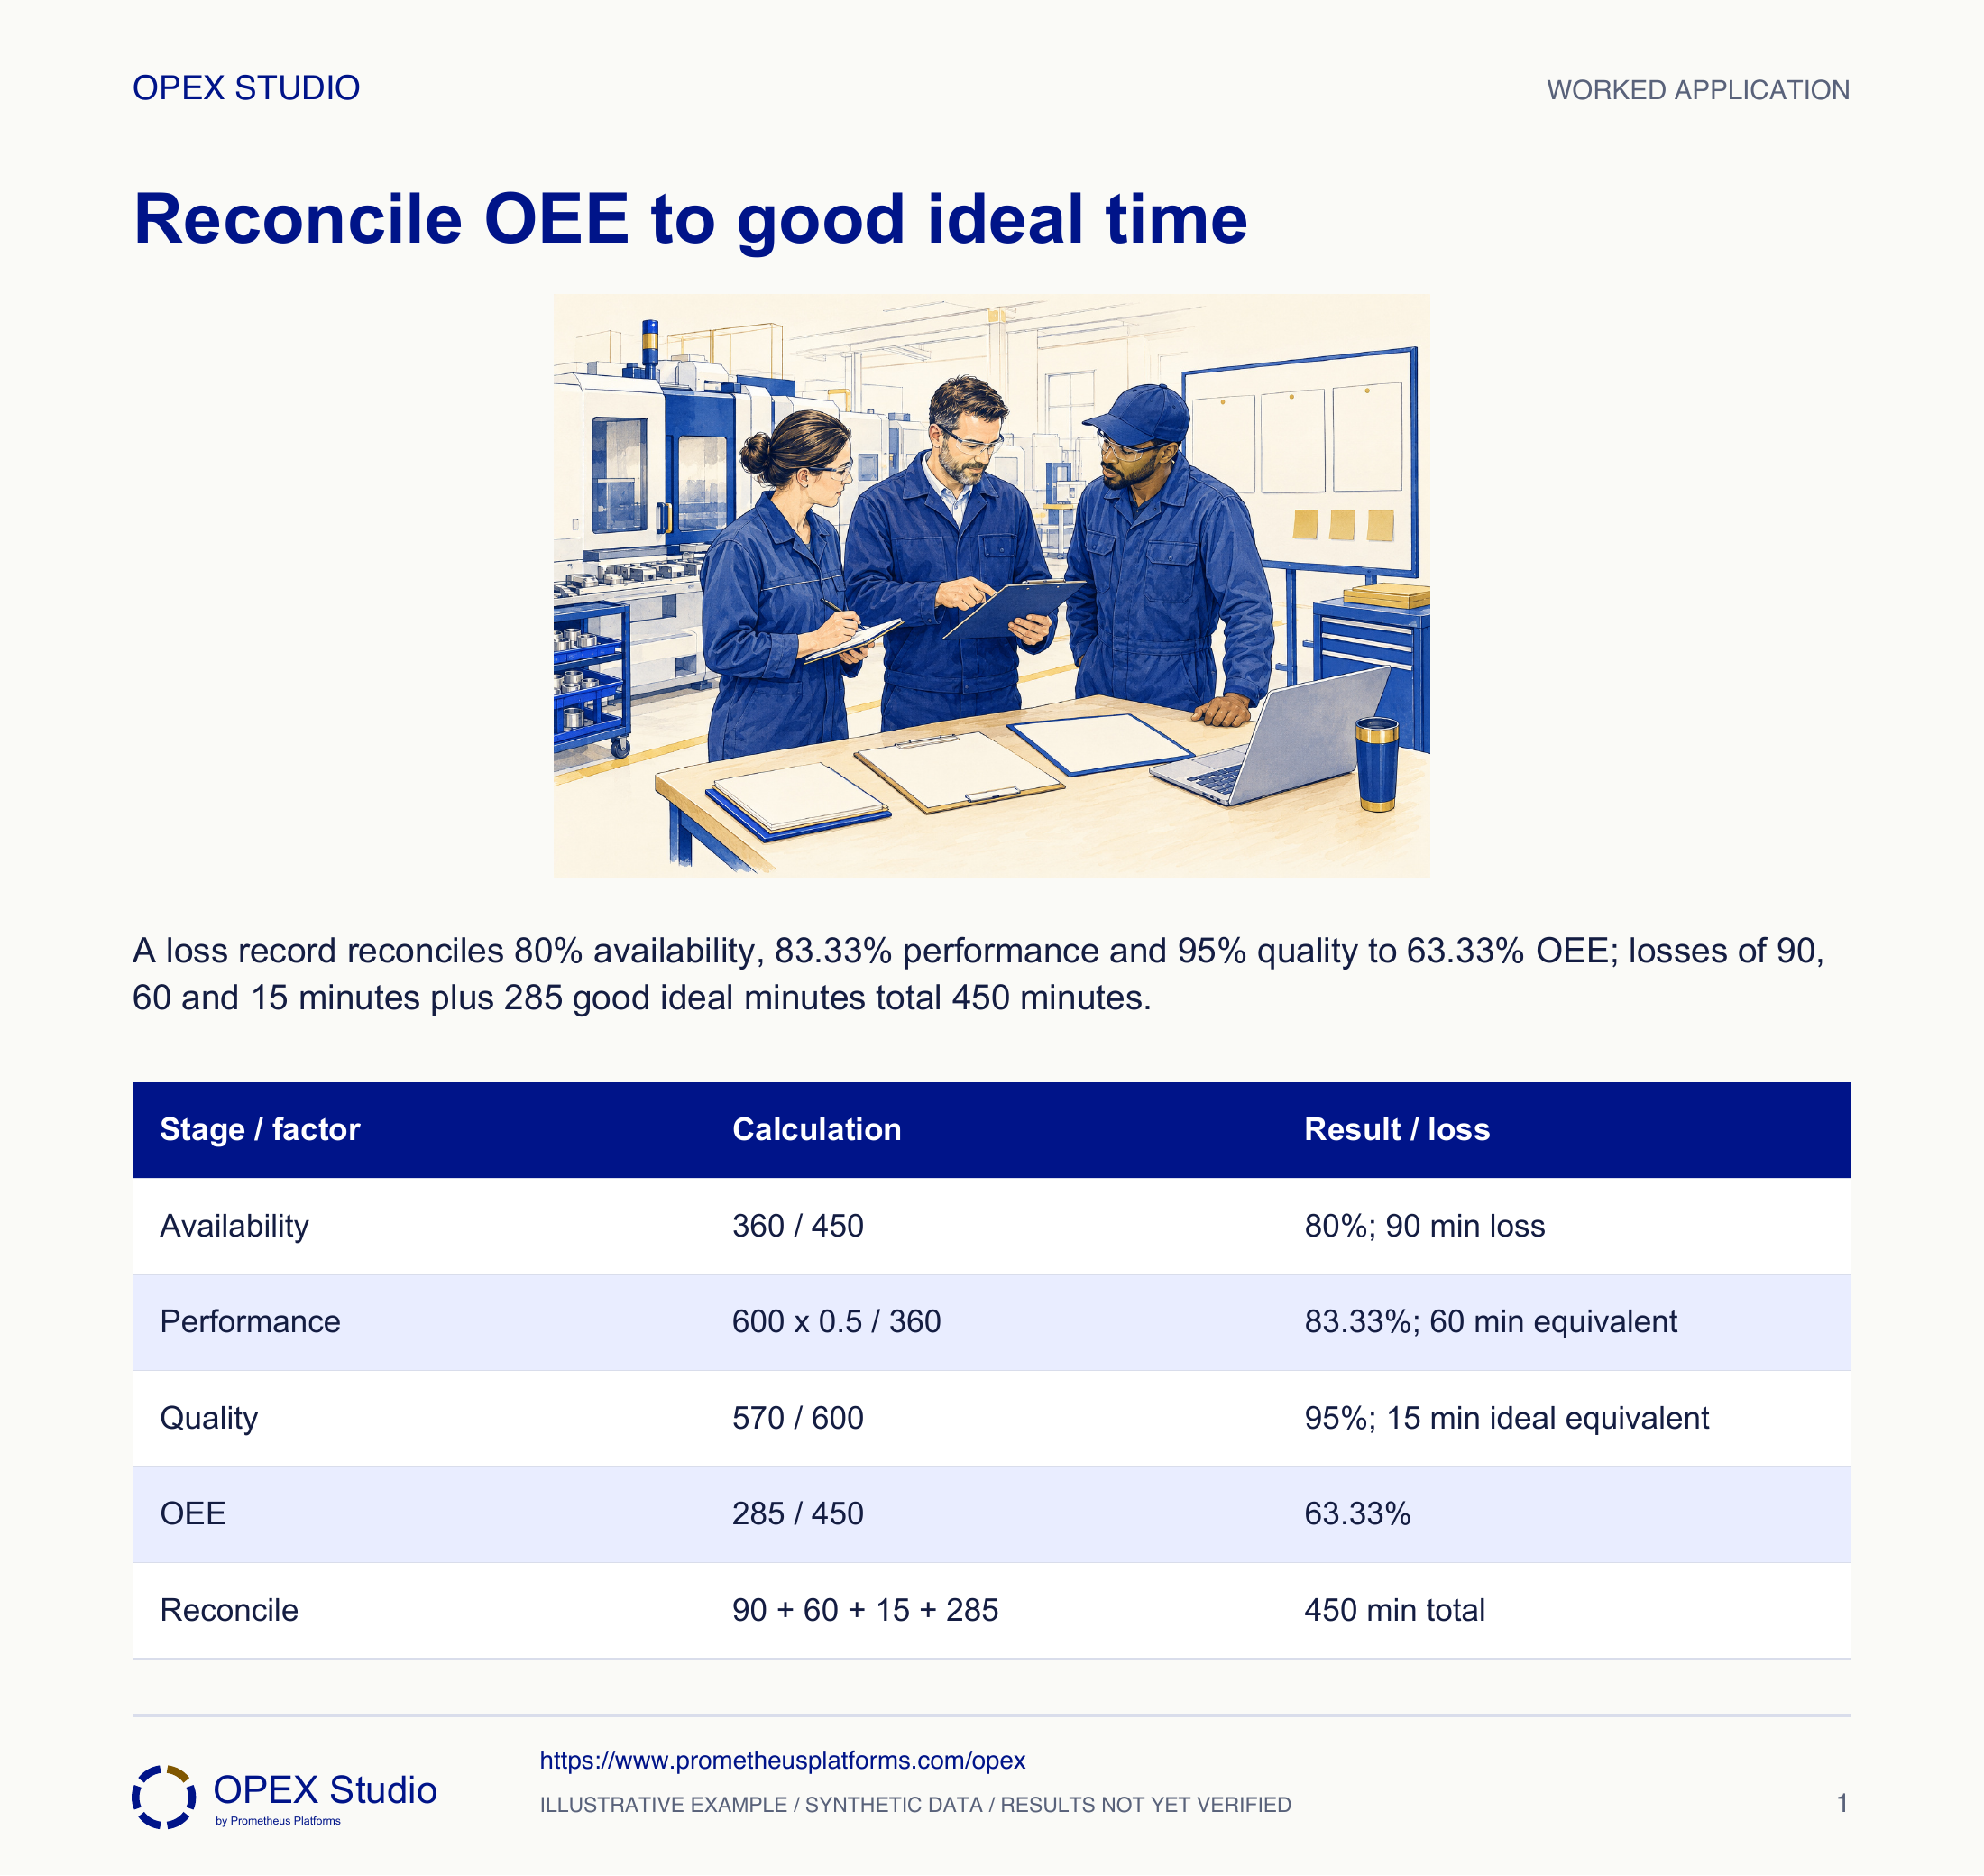
| Stage / factor | Calculation | Result / loss |
|---|---|---|
| Availability | 360 / 450 | 80%; 90 min loss |
| Performance | 600 × 0.5 / 360 | 83.33%; 60 min equivalent |
| Quality | 570 / 600 | 95%; 15 min ideal equivalent |
| OEE | 285 / 450 | 63.33% |
| Reconcile | 90 + 60 + 15 + 285 | 450 min total |
The 30 non-first-pass units include 20 subsequently reworked and accepted. A colleague proposes changing first-pass good from 570 to 590.
Keep first-pass quality at 570 / 600 = 95% for this defined original pass and record rework/recovery separately. Clarify how any rework resource/time enters the relevant reporting scope.
Recovery changes disposition, not first-pass history. Mixing scopes can count output or time twice.
Retain the original counts, rework identities, subsequent disposition and approved time-accounting rule.
New fictional record: 480 planned minutes, 400 run minutes, 800 total units, 750 first-pass good and an approved ideal cycle of 0.4 min/unit. Twenty failed units are later recovered; do not change the original first-pass count.
| Input | Value |
|---|---|
| Planned / run | 480 / 400 min |
| Total / first-pass good | 800 / 750 units |
| Ideal cycle | 0.4 min/unit |
| Later recovered | 20; separate disposition |
Availability is 400 / 480 = 83.33%; performance is 800 × 0.4 / 400 = 80%; quality is 750 / 800 = 93.75%. OEE is 62.5%, also 300 good ideal minutes /480.
Availability loss is 80 minutes; performance loss is 400 minus 320 = 80 minutes; quality ideal loss is 320 minus 300 = 20 minutes. These plus 300 good ideal minutes total 480.
The 20 later recovered units do not change 750 first-pass good. The loss categories suggest questions, not a diagnosis or proof of customer throughput improvement.
| Measure | Worked result |
|---|---|
| Availability / performance / quality | 83.33% / 80% / 93.75% |
| OEE | 62.5%; 300 / 480 |
| Losses | 80 + 80 + 20 = 180 min |
| Reconcile | 180 + 300 = 480 min |
| Recovery | 20 separate; first-pass good remains 750 |
Which time is planned, run and ideal?
Where do the 15 quality-loss minutes come from?
Can both OEE paths agree?
What event evidence is needed before choosing a repair?
Calculate factors and direct good-ideal-time ratio independently, then use their agreement as a reconciliation check.
Owner: Performance-data owner with production, quality and maintenance
Record: Controlled shift loss record linked to time and unit events
Review: At loss review and after a targeted countermeasure trial
Evidence: Consistent definitions, reconciled counts/time and observed loss mechanisms
Repair data scope or investigate event records before changing targets or attributing causes.
Availability × performance × quality and loss categories
Method reference; original OPEX scenario and diagram are synthetic teaching content, not source case results.Read online without signing in, or take this lesson into your next team conversation.
Topic pack · 10 pages · Reviewed teaching edition.
Read the lessons online or use these PDFs to prepare, practise and review with your team. No sign-in needed.
Case objectives, demonstration plans, debriefs, common mistakes and application checks across all 81 workplace cases and method lessons.
Download Facilitator guide PDF · 166 pages · 65.1 MBPrintable case worksheets, blank observation records and five calculation exercises; answers are separate.
Download Learner workbook PDF · 169 pages · 10.7 MBReasoned sample responses, worked calculations and coaching guidance; fictional examples are clearly labelled.
Download Answer key and coaching notes PDF · 105 pages · 8.5 MBThe native method mechanisms and worked applications for all 68 detailed lessons, in a separate bookmarked portrait reference.
Download Method and application reference PDF · 141 pages · 10.2 MBFive illustrated system chapters: 15 Flare concept maps and 26 original workplace teaching cards, with links to all 81 supporting cases and method lessons.
Download Illustrated systems atlas PDF · 69 pages · 55.8 MBExplore this connected method and its separate application conditions.
Explore the connected method →Explore this connected method and its separate application conditions.
Explore the connected method →Explore this connected method and its separate application conditions.
Explore the connected method →Explore this connected method and its separate application conditions.
Ask OPEX Guide how to apply this learning to your situation. Describe the expected condition, the gap and the evidence you have. Review its suggestions with the people doing the work before deciding on a change.
Explore your question with OPEX Guide →